Choosing among the top prototype machining companies can shape a product’s first real test. A reliable partner must do more than cut metal accurately. It should understand design intent, material behavior, surface requirements, and production risk.
Prototype Machining often involves tight deadlines and changing specifications. A capable supplier can review CAD files, identify weak features, and suggest practical design improvements. Look for evidence of experience with aluminum, stainless steel, titanium, engineering plastics, and difficult geometries. Machine capability matters, but inspection discipline matters just as much. Ask about coordinate measuring machines, dimensional reports, surface-finish checks, and traceable material certificates.
Communication is equally important. Clear updates can prevent a small tolerance issue from becoming an expensive delay. Some global suppliers offer rapid quoting, multilingual support, and shipping coordination. These services are useful, but they should not replace technical evaluation. Published accuracy figures may look impressive. They do not always explain performance across different materials, batch sizes, or complex parts.
A thoughtful comparison should examine lead times, tooling needs, revision control, confidentiality practices, and quality records. Request sample work when possible. Review the supplier’s response to unclear drawings. That response reveals practical competence.
No company is perfect. Even experienced teams can miss a hidden tolerance conflict or underestimate finishing time. Buyers should leave room for technical discussion and one more design review. The strongest machining partner is not always the cheapest or fastest. It is the company that delivers measurable quality, explains limitations honestly, and supports a prototype through its next development stage.
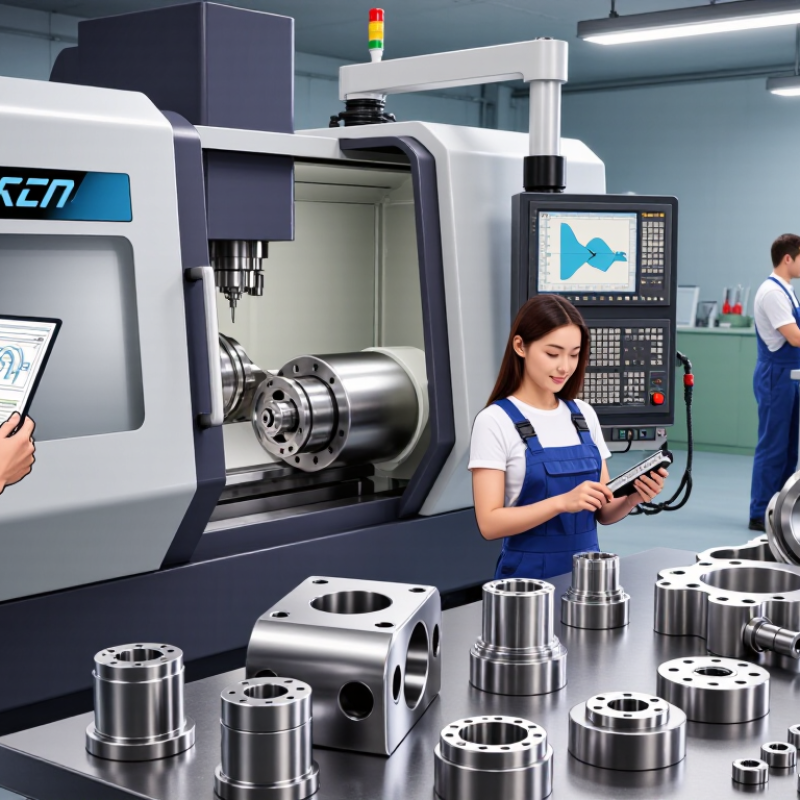
Prototype machining companies turn digital designs into physical parts for fit, function, and manufacturing checks. They commonly use CNC milling and turning to shape metals or plastics from CAD files. Before cutting material, a capable team reviews dimensions, tolerances, wall thickness, and features that may be difficult to machine. It may suggest small design changes, then produce a sample for inspection. That matters. A prototype can expose a poor fit or a sharp edge before a larger production run begins.
Tips: Share a current drawing, material preference, and critical dimensions. Ask how inspection results will be reported. Clarify whether the quoted schedule includes finishing and shipping. These details reduce guesswork, though they cannot remove every delay.
For global buyers, clear communication is as important as machine capacity. Confirm units, revision numbers, surface-finish expectations, and delivery terms in writing. Request measurements for the features that matter most, such as a bore diameter or mounting-hole spacing. A low quote may exclude useful checks or finishing steps, so compare scope, not price alone. Even a carefully reviewed prototype may need another iteration; that is normal, and sometimes the first design assumptions were simply wrong.
Global buyers evaluate prototype machining suppliers through evidence, not attractive quotations. They compare tolerance control, material traceability, inspection methods, and response speed. A supplier should provide sample inspection reports, calibrated equipment records, and clear dimensional assumptions. The ISO Survey 2023 recorded more than 1.2 million ISO 9001 certificates worldwide, but certification alone does not prove machining capability. Ask for recent examples involving similar alloys, wall thicknesses, and geometric tolerances.
Lead time needs careful testing. A reliable supplier separates programming, material purchasing, machining, inspection, and shipping dates. This detail exposes hidden delays. Deloitte’s 2023 Global Chief Procurement Officer Survey identified cost reduction as a leading procurement priority, yet low price can conceal rework, poor packaging, or unstable process control. Buyers should request a first-article plan and a defined correction process. Small details matter.
Communication is also measurable. Can engineers flag an impossible radius before cutting metal? Do they confirm datum references in writing? According to the UNCTAD Review of Maritime Transport 2023, maritime shipping carries over 80% of global merchandise trade by volume, making export packaging and documentation important. Still, supplier evaluation is rarely perfect. A polished report may reflect one successful batch, not consistent performance. Run a small pilot order, inspect critical features independently, and record what went wrong.
Suggested allocation of evaluation points across key supplier-selection criteria.
This 100-point framework is a practical starting point, not survey data. Buyers can adjust the weights to reflect part complexity, application requirements, and project priorities.
Prototype machining companies support design teams by turning CAD models into physical parts quickly. CNC milling creates flat faces, slots, and complex contours, while turning suits shafts, sleeves, and other round components. Drilling and tapping add functional holes for fasteners. For thin walls or deep pockets, tool access can affect both cost and accuracy. A feature that looks simple on screen may need a design adjustment.
Material choice changes machining behavior. Aluminum is lightweight and generally machines efficiently, making it useful for housings and brackets. Stainless steel resists corrosion but can generate more heat during cutting. Engineering plastics reduce weight and may suit insulating or low-friction parts, though they can deform under clamping. Ask about available grades, stock thickness, and material certificates. Surface finish and tolerance targets matter, too; specifying tighter limits everywhere can add time without improving the part’s function. That trade-off is easy to overlook.
Tips: Share the part’s intended use, critical dimensions, and expected quantity with the machinist. Mark only essential tolerances on the drawing. Request inspection results for key features, such as bore diameter or hole spacing. If the first prototype reveals a weak wall or awkward tool path, revise the design before ordering more. The first version is rarely perfect.
For global buyers, prototype machining quality begins with a controlled process, not a polished website. Experienced suppliers review drawings, materials, surface finishes, and critical dimensions before cutting metal. They should confirm unclear tolerances early. Details matter.
A reliable shop matches inspection tools to the part. Digital calipers suit general dimensions, while micrometers verify tighter features. Coordinate measuring machines check hole positions, profiles, and complex geometries. Surface roughness testers help confirm functional finishes. Inspectors should record actual readings, not only mark parts as acceptable. Material certificates and heat-treatment records also support traceability.
Tolerance control needs practical judgment. A prototype may require ±0.01 mm on a bearing seat, but that precision can be unnecessary elsewhere. Overly tight tolerances often increase cost and production time. Skilled engineers identify critical features and recommend realistic limits. Measure twice. Then question the result.
Inspection reports should include drawing revisions, instrument identification, calibration status, measured values, and nonconformance notes. Photos of difficult features can clarify findings for overseas teams. First-article inspection is useful, yet it cannot replace process discipline during later batches. Human error remains possible, especially when datums are vague or inspection access is limited. Even experienced teams can miss a small burr inside a cross-drilled hole. That weakness deserves review, not concealment. Reliable communication, documented evidence, and repeatable checks give buyers a clearer basis for approving prototypes.
Use this supplier-evaluation guide to compare machining capabilities and quality practices. Tolerances and inspection requirements depend on the part drawing, material, geometry, process, and agreed acceptance criteria; the figures below are not guarantees for every part.
| Evaluation Area | Relevant Standard or Reference | Practical Benchmark for Buyers | Inspection Evidence to Request |
|---|---|---|---|
| Quality management system | ISO 9001 | Check whether the supplier’s quality-management-system certificate is current, covers the relevant site, and includes the applicable manufacturing activities. ISO 9001 certification does not by itself certify an individual part. | Current certificate, issuing certification body, site scope, and documented procedures for handling inspection records and nonconformities. |
| General dimensional tolerances | Drawing requirements; ISO 2768 where explicitly specified | Confirm the tolerance class and which dimensions it applies to. ISO 2768 is not automatically applicable unless referenced by the drawing or purchase documentation. | Ballooned drawing or inspection plan showing measured dimensions, nominal values, tolerances, and results. |
| Limits, fits, and shafts or holes | ISO 286 series | For specified ISO fits, verify the tolerance designation and size range on the drawing rather than relying on a generic machining-accuracy claim. | Calibrated micrometer, bore gauge, plug gauge, or other suitable measurement results for the specified fit features. |
| Geometric tolerancing | ASME Y14.5 or ISO GPS standards, as specified by the drawing | Agree on the governing drawing standard, datums, and interpretation before production. ASME and ISO conventions should not be assumed interchangeable in every application. | Inspection results tied to the drawing’s datum reference frame, with the measurement method identified for critical geometric controls. |
| Prototype tolerance capability | Part drawing and supplier process capability | Ask for a part-specific capability review. A tolerance such as ±0.10 mm may be practical for many milled features, but achievable limits vary with feature size, material, geometry, setup, and process. | Written feasibility review identifying critical dimensions, proposed process, inspection method, and any features requiring agreement or redesign. |
| Surface texture and finish | Surface-texture callouts on the engineering drawing | Specify the required parameter and limit, such as Ra, when surface finish matters. Do not assume a particular finish from a general statement such as “CNC machined.” | Surface-roughness tester results for specified areas, or a documented visual inspection method where the requirement is visual. |
| Coordinate measurement | ISO 10360 series for coordinate measuring machine performance | For complex geometry or tight positional requirements, confirm that the measurement method and equipment are suitable for the part’s size, tolerance, and datum scheme. | CMM inspection report with feature references, measured values, acceptance limits, and equipment identification. |
| Measurement equipment and calibration | ISO 9001 measurement-resource controls; ISO/IEC 17025 for accredited calibration laboratories | Check that measuring equipment is controlled and calibrated at suitable intervals. ISO/IEC 17025 applies to competent testing and calibration laboratories, not as a general machining-company certification. | Calibration status or certificates for instruments used on critical features, including identification and due dates. |
| Material verification and traceability | Purchase-order and drawing requirements; applicable material specifications | Define the required alloy or material grade and whether lot-level traceability or material certification is needed, especially for regulated or safety-critical applications. | Material test certificate or supplier certificate, material and lot identification, and traceability records where required. |
| First-article and in-process inspection | Customer-defined inspection plan; AS9102 when required for applicable aerospace work | Agree on which features receive first-piece, in-process, and final inspection. AS9102 is an aerospace first-article inspection standard and should not be presumed to apply to every prototype order. | First-article report when specified, in-process checks for critical features, and final inspection results linked to the drawing revision. |
| Nonconformance and corrective action | Supplier quality procedures and purchase-order requirements | Confirm that out-of-tolerance parts are identified, segregated, and reported before any repair, rework, or concession is made. | Nonconformance report, documented disposition, customer approval where required, and corrective-action records for recurring issues. |
| Export, packaging, and delivery documentation | Purchase-order terms and destination-country requirements | Agree on delivery terms, packaging, labeling, customs documentation, and any required declarations before shipment. | Packing list, commercial invoice, shipment tracking, and any agreed inspection or material documents. |
A low prototype quote can hide costs for setup, finishing, inspection, or shipping. Compare prices against the same material, quantity, tolerances, and surface requirements. Ask for a line-item quotation, including any charges for design changes. Details matter.
A capable machining partner should flag unclear dimensions before production, not after parts arrive. Share a controlled drawing revision and name one contact for approvals. Agree on update intervals and response times across time zones. A short written recap after each decision reduces avoidable rework. Still, messages can be missed, so record important changes in the drawing or purchase documents.
Lead time should separate engineering review, machining, finishing, inspection, and transit. Ask which dates are estimates and which depend on your approval. A rushed schedule may leave little room for a revised toolpath or failed inspection.
International delivery adds variables: request the carrier, tracking plan, packaging method, and estimated transit window. Confirm who prepares shipping documents and who handles destination charges or import requirements. Requirements vary by destination, so buyers should verify them with their logistics provider. Even careful forecasts can slip. A few days of buffer can protect a launch plan, though it will not fix every delay.
It turns CAD designs into physical parts for fit, function, and manufacturing checks. A sample can reveal a poor fit or sharp edge before larger production.
Milling makes flat faces, slots, and complex contours. Turning suits round parts like shafts and sleeves. Drilling and tapping create functional holes.
Common options include aluminum, stainless steel, and engineering plastics. Aluminum is lightweight, while stainless steel resists corrosion. Plastics can deform under clamping. Details matter.
Share a current drawing, revision number, material preference, quantity, and critical dimensions. Include the part’s intended use. Guesswork can still happen.
No. Mark tight limits only where they affect function, such as a bore diameter or mounting-hole spacing. Extra precision can add time without helping the part.
Ask whether the price includes setup, finishing, inspection, design changes, and shipping. Compare quotes with the same scope, not price alone. Not always obvious.
Ask for separate estimates for review, machining, finishing, inspection, and transit. Confirm which dates depend on your approval. Add a few days of buffer.
Confirm the carrier, tracking plan, packaging, transit estimate, and who prepares shipping documents. Check destination charges and requirements with your logistics provider. Plans can slip.
Not always. Inspection may reveal a weak wall or awkward tool path. Revise the design if needed; first assumptions are sometimes wrong.
Prototype Machining companies help turn product concepts into accurate physical parts for testing, design validation, and small-scale production. They may work with processes such as CNC milling and turning, sheet metal fabrication, or additive manufacturing, depending on the part’s shape and requirements. For global buyers, choosing a supplier involves more than comparing prices: buyers should assess technical expertise, material options, production capacity, communication, and the ability to meet project specifications.
Quality depends on clear tolerances, suitable inspection methods, and consistent documentation. Buyers should confirm how dimensions and surface finishes are checked, and whether the supplier can provide inspection reports when needed. Pricing should be evaluated alongside lead times, shipping arrangements, and the supplier’s process for handling design changes or delays. A dependable Prototype Machining partner communicates clearly, explains trade-offs, and coordinates international delivery so that parts arrive ready for evaluation.